Material is the least audited purchase in most insole workshops. Buyers inspect machines carefully and materials casually, even though a material that behaves differently from the previous batch will change every pair produced from it, whatever the equipment.
The reason is practical. A machine arrives as an object with a serial number and a manual; material arrives as sheets in a carton with a label that may or may not be accurate. Auditing it requires a method rather than a conversation, and most buyers have never been shown one.
This article sets out that method: what to test on receipt, what to record, how to store material so it behaves consistently, how to approve a sample properly, and what to do when a batch does not match. It is written from the position of a manufacturer that buys material in volume and lives with the consequences.
Why material is invisible until it fails
Material faults rarely announce themselves at delivery. A sheet with a slightly different stiffness forms acceptably, produces pairs that look right, and reveals itself three weeks later when a customer reports that the arch has flattened or the edge has lifted.
By then the batch is in production, the pairs are in the field and the cause is difficult to isolate. The workshop suspects the operator, the operator suspects the machine, and the actual variable — a supplier change or a storage problem — is not on anybody’s list.
The remedy is to make material visible at receipt. A short, repeatable check creates a record that turns an invisible variable into a document, and a document can be compared across batches.
Testing a batch on receipt
Four checks cover most of what matters, and none of them requires a laboratory. They take a few minutes per batch and produce a record that will be worth its cost the first time something goes wrong.
Thickness, measured consistently. The point is not the absolute figure but the variation across a sheet and between sheets in the same carton. Measure at the same positions every time, with the same instrument, and record the spread rather than a single number.
Stiffness, compared against a reference. A simple three-point bend on a strip cut to a standard size, compared by feel and by deflection against a retained reference strip, reveals a grade that is out of family. It is not a laboratory measurement; it is a comparison, and comparison is what a workshop needs.
Surface and colour. A change in surface texture or colour can indicate a different supplier, a different production run or a storage problem. Both matter, and neither is obvious unless someone looks at a new batch next to an old one.
A test form. Form one pair with the standard routine and compare it against a retained reference pair. This is the only check that measures how the material actually behaves in your process, and it is the one most often skipped.
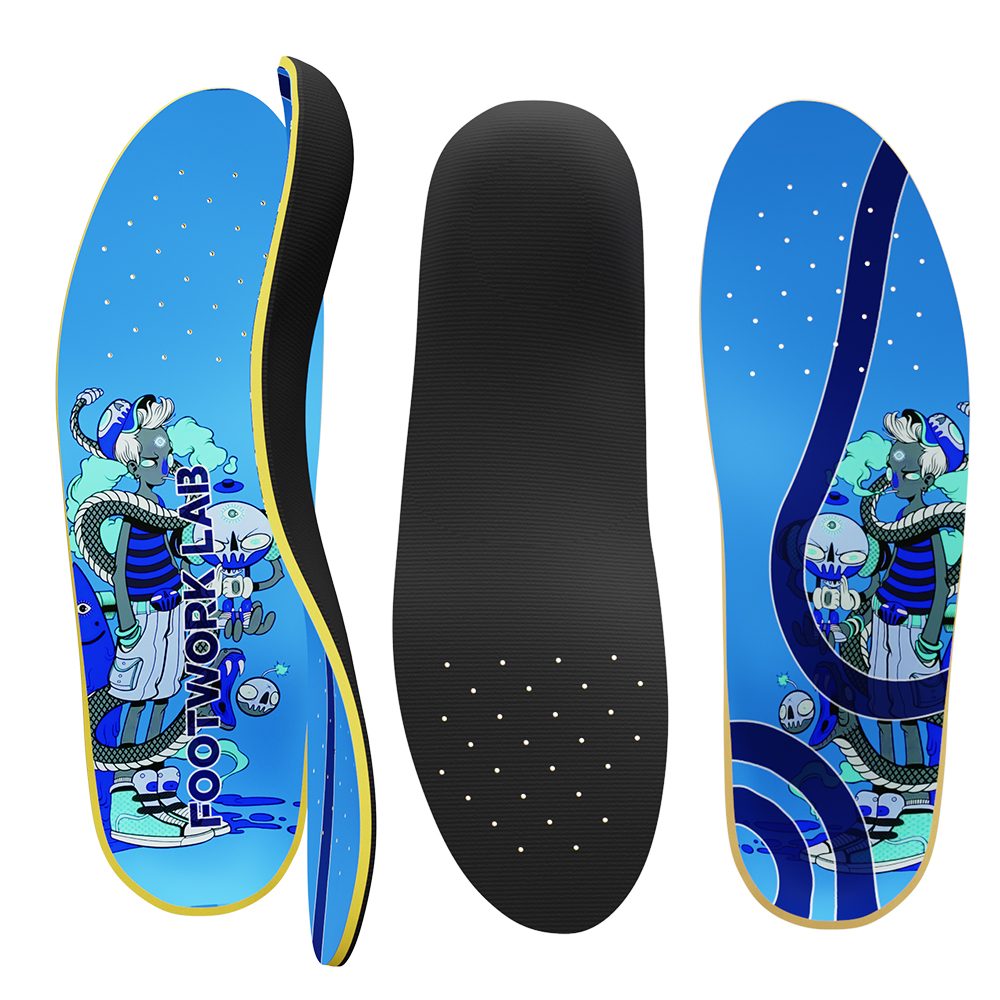
The fourth check is the one that most often gets skipped, because it consumes material: form a pair and keep it. A retained pair from each approved batch is the only artefact that records how that material behaved in your own process, and it is the reference that settles an argument six months later when a customer returns a pair and nobody can remember what changed.
None of these checks requires a laboratory, and all of them require consistency. Measuring at different positions each time produces numbers that cannot be compared, which is worse than no numbers at all because it creates false confidence.
Storage discipline as part of the process
Material changes in storage. Sheets absorb moisture, some foams degrade under ultraviolet light, and cartons stacked under pressure deform in ways that show up in the formed product. Storage is therefore part of the process, not an administrative afterthought.
The practical rules are few. Keep material sealed until use, store flat rather than on edge, keep cartons off the floor in humid climates, and rotate stock so that the oldest material is used first. Record the date a carton was opened, because the clock that matters starts then.
Temperature matters less than humidity for most materials, but both matter if the workshop is unheated or if material is stored in a room that swings with the seasons. Material that has spent a winter in a cold store behaves differently on the first day it is used, and the difference is often attributed to the machine.
Where a workshop holds several grades, physical separation prevents the most common error in small production: using the right grade in the wrong place. Labelled shelving with a clear position for each grade costs almost nothing and removes a whole category of mistake.
There is a commercial dimension to storage that is easy to overlook. Material bought in bulk to obtain a better unit price can deteriorate before it is used, and the saving is quietly consumed by rejected batches. For a workshop with modest volume, buying less more often is often cheaper than buying well, even at a higher unit price.
Samples and approval, done properly
Sample approval is where a buyer establishes what “the same material” means. Done badly, it produces a colour swatch and a verbal reassurance. Done properly, it produces a reference that can be tested against every future delivery.
The reference should include the physical sample, the batch number, the date received, the thickness and stiffness results from the receipt checks, and a retained formed pair. Together these allow a future batch to be compared on the same terms rather than on memory.
Approval should also state the tolerances the buyer will accept, in writing. A supplier who knows that a thickness variation beyond a certain spread will be rejected tends to control it; one who has never been told has no reason to.
For buyers ordering insoles rather than material, the same logic applies one level up. A specification that names the material family and grade, and a retained reference pair from the approved batch, gives the factory a clear standard and the buyer a way to verify it.
Suppliers should also be asked how they handle a claim. A supplier who replaces a doubtful batch without argument is worth a premium; one who requires the buyer to prove the material was stored correctly is technically within their rights and practically difficult to work with. Both behaviours are visible in a single conversation before the first order, and the answer predicts how the second year will feel.
Documentation worth asking for
Three documents make a material supply auditable. The first is a batch or lot number on the packaging, which is the thread that connects a finished pair back to a delivery.
The second is a certificate of analysis or a specification sheet stating the nominal properties of the grade. Buyers do not need to verify every property themselves; they need to know what the supplier claims, so that a deviation can be discussed in the supplier’s own terms.
The third is a statement of what changed, if anything, between batches. Suppliers who reformulate quietly create problems for their customers, and a supplier who volunteers a change before shipment is worth keeping.
Where documentation is thin, the receipt checks become more important rather than less. A workshop that cannot rely on paperwork has to rely on measurement, and measurement requires the record described above.
The approval record should also name who approved it. A sample approved by a person who has since left, with no note of what they were checking, is a sample nobody can defend. Naming the approver and the criteria turns a physical object into a decision with a rationale.
When a batch does not match
The first response should be to isolate, not to argue. Quarantine the batch, keep the reference and the test pair, and stop production from it until the difference is understood. Continuing production while a question is open converts a material issue into a field issue.
The second response is to describe the difference in measurable terms. “It feels different” invites a disagreement; “the formed arch is shallower at the same settings, the thickness spread is wider, and the surface is glossier” invites an explanation.
The third is to decide the disposition in writing: reject, accept with an adjusted routine, or accept for a non-critical product. Each of those is legitimate; what is not legitimate is accepting silently and hoping the pairs behave.
Recording the outcome, including the supplier’s response, builds a history that changes future behaviour. Suppliers respond to buyers who document, because documentation is what makes a claim credible.
A further document worth requesting is the supplier’s own handling instruction: storage temperature, humidity range and shelf life. Suppliers who cannot state these are usually suppliers who have not thought about how their material behaves after it leaves the factory, and that gap becomes the buyer’s problem in the third month of a humid season.
Buyers should also decide what they will do with a batch that is acceptable but different: reserve it for a non-critical product, adjust the routine for it, or return it. Having that decision pre-made prevents the common pattern of using a doubtful batch because it is already paid for.
Single source and dual source
Single sourcing gives consistency and negotiating simplicity; dual sourcing gives resilience and a comparison point. Most workshops need both, in a ratio that depends on how critical the material is.
For the main shell material, a single approved source with a retained reference is usually better than two sources used interchangeably, because two sources mean two behaviours and the workshop cannot tell which one produced a given batch. Where resilience matters, keep a second source approved but not in routine use.
For consumables — adhesives, covers, packaging — dual sourcing is easier because the properties are simpler and the consequences of variation are smaller. Even there, approval should include a test pair rather than a visual check.
The worst arrangement is several sources used randomly, which is common in workshops that buy on availability. The result is a process that varies for reasons nobody can trace, and a quality conversation that never reaches a conclusion.
It also helps to decide what the workshop will do with material that is acceptable but not identical: reserve it for sample pairs, use it for a product where the property matters less, or hold it until the supplier confirms. Having that decision written down prevents the common pattern of using a doubtful batch because it has already been paid for and the order is due.
How we handle it in our own plant
Our production runs material in batches against approved specifications, with retained reference pairs from each approved batch and a record of what was used for each production run. When a customer’s specification names a material, that name is what the batch is built from, and a substitution is a conversation rather than a decision.
For buyers ordering insoles to specification, the practical implication is that material questions belong in the specification, not in a later email. Naming the grade, the thickness range and the finish gives the factory something to hold, and gives the buyer something to compare against when a reorder arrives.
Material discipline is unglamorous and it compounds. A workshop that has a batch log, a retained reference and a written approval routine can trace almost any complaint to its cause within an afternoon, and that ability is worth more than the paperwork costs.
Material auditing is also a negotiating position. A buyer who can describe a batch in measurable terms, and who has a retained reference to compare against, is a buyer whose complaints are taken seriously. The paperwork is not bureaucracy; it is the mechanism by which a small workshop has a conversation with a large supplier on equal terms.
None of it requires a quality department. It requires one page per batch, four checks, one retained pair and a signature, and it takes less time than the argument it prevents.
Frequently asked questions
Do I need laboratory equipment to audit insole material?
No. Thickness measurement at marked positions, a three-point bend compared against a retained strip, a visual check against a previous batch and a test form using your standard routine cover most of what matters in a workshop.
How long should material be stored before use?
As short a time as your ordering allows, in sealed packaging, stored flat and rotated so the oldest stock is used first. Record the date a carton is opened, because moisture uptake and ageing begin then.
What should a material sample approval include?
The physical sample, the batch number, the date received, the receipt check results and a retained formed pair. Together they let a future delivery be compared on the same terms rather than against memory.
What do I do if a new batch behaves differently?
Quarantine it, keep the reference and the test pair, and describe the difference in measurable terms before contacting the supplier. Then decide the disposition in writing: reject, accept with an adjusted routine, or reserve it for a non-critical product.
Should I use two material suppliers?
Keep a second source approved for resilience, but avoid using two sources interchangeably for the main shell material. Two sources mean two behaviours, and a workshop cannot tell which one produced a given batch.
What material details belong in an insole specification?
The material family and grade, the thickness range, the surface finish and the retained reference. Naming those gives the factory something to hold and the buyer something to compare a reorder against.
What is your minimum order for insoles produced to specification?
Two hundred pairs, mixable across models and sizes, with samples dispatched within three days of specification approval. ODM and OEM work are both accepted.
What we would do next
Start a material log this week: one page per batch, four checks, one retained pair. It is the cheapest quality system available and the only one that will explain a problem six months from now. Our insole categories page shows the ranges we build and the FAQ page covers order terms, samples and ODM work.
This article is intended for professional and educational reference. It is not medical advice. Foot assessment equipment produces measurements and images; clinical interpretation and any decision about care remain the responsibility of a qualified professional. Certification scope is limited to the documentation we hold: European Union certification and ISO quality system certification.